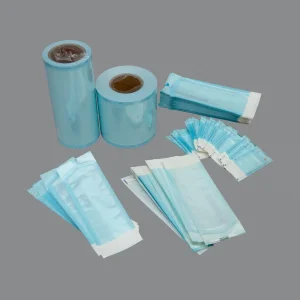
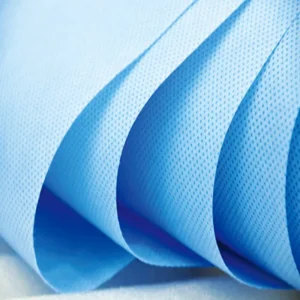
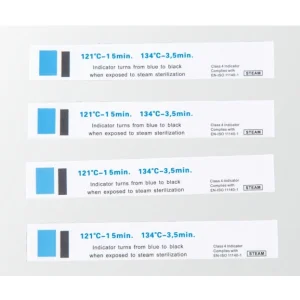
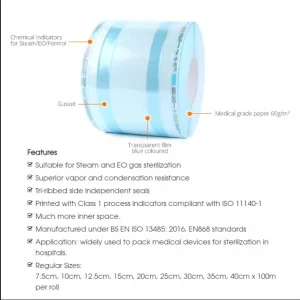
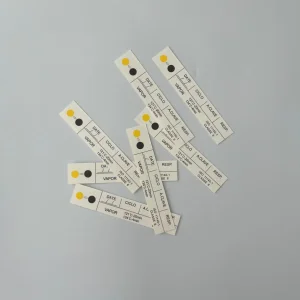
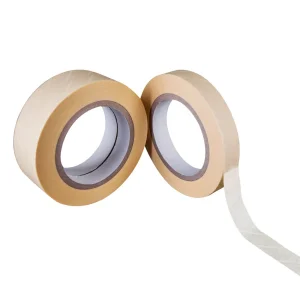
Explore our primary line of advanced medical grade sterilization packaging and wrapping supplies.
A globally trusted backbone for specialized high-tech medical and industrial materials.
Guangdong Onyx Medical Co., Ltd. is a leading national high-tech enterprise specializing in the research, development, production, and supply of advanced materials for the personal care, medical, and electronics industries. Since its establishment, the company has adhered to a core philosophy of innovation and quality, dedicated to providing high-quality products and solutions to customers worldwide. Located in Guangdong, China, the company operates a modern manufacturing facility covering over 60,000 square meters, equipped with three Class 100,000 cleanrooms and more than 30 PLC-controlled automated production lines. This state-of-the-art infrastructure ensures that every production process meets the highest levels of precision and safety, adhering to international standards.
Modern Manufacturing Facility
Class 100,000 Sterile Environments
PLC-Controlled Automated Production
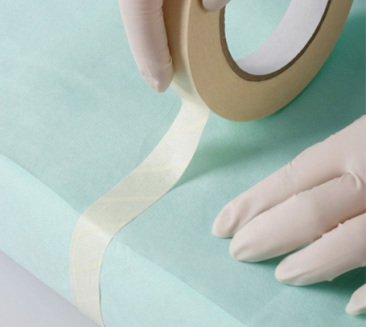
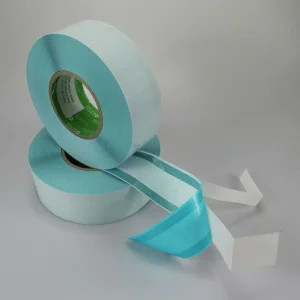
Medical Sterilization Tape Series
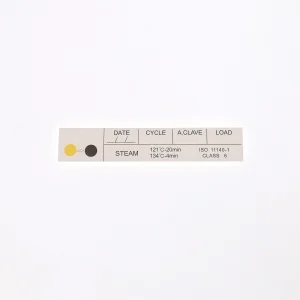
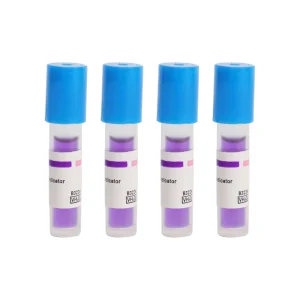
Medical Sterilization Monitoring Series
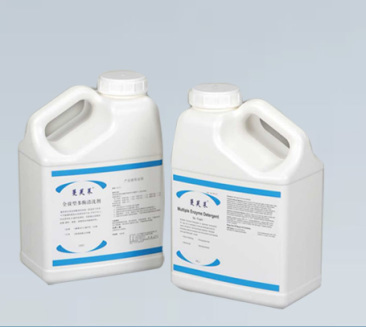
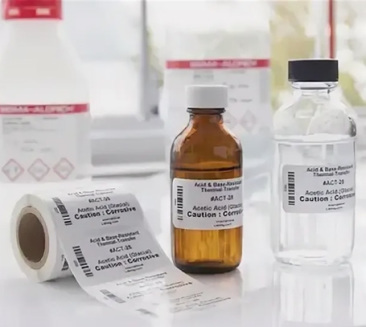
Medical Detergent Series
Addressing complex regulatory and functional demands across diverse global markets.
Guangdong Onyx Medical is structured into multiple specialized divisions, each committed to addressing the unique needs of its respective industries:
The company develops advanced biomaterials and medical sensors widely used across various healthcare sectors, including diagnostic equipment, vital signs monitoring systems, and patient care products. Onyx Medical is dedicated to continuous innovation to enhance patient outcomes and improve the quality of care.
Onyx Medical provides high-quality materials for personal care products, particularly in the infant diaper and hygiene product markets. The company ensures that its products offer superior comfort, safety, and moisture absorption, catering to the growing demand in global markets.
Onyx Medical manufactures high-precision medical sensors and control consumables that are widely used in critical medical devices. These products enhance the reliability and effectiveness of health monitoring systems, providing safer and more efficient technology support for the healthcare industry.
The company is at the forefront of research and development in biocompatible materials, with a particular focus on regenerative medicine and drug delivery systems. Onyx Medical is committed to driving breakthroughs in materials science, continuously introducing innovative products that improve patient care.
Onyx Medical also focuses on the development of next-generation electronic materials for use in consumer electronics and industrial applications. These materials are designed to offer superior performance and durability, meeting the growing demands of the global electronics market.
Pioneering sustainable, intelligent, and ultra-barrier packaging technology for modern hospitals.
Transitioning from traditional petrochemical non-wovens to bio-based SMS and SMMS structures that reduce hospital carbon footprints without compromising sterile barrier integrity or tear resistance during heavy surgical instrument loading.
Integrating real-time molecular and nanotech color-changing indicators directly into wrap fibers, enabling instant visual verification of steam, ethylene oxide (EO), and hydrogen peroxide plasma sterilization efficacy.
Leveraging electrospun nanofiber layers to establish microscopic tortuous paths that block bacterial spores and viruses while optimizing steam penetration and rapid post-sterilization drying cycles.
Meeting the stringent expectations of international healthcare networks, GPOs, and distributors.
International medical institutions demand zero-interruption supply chains. Onyx Medical utilizes automated inventory forecasting, multi-port logistics dispatch, and buffer stock programs to protect global partners against geopolitical and logistical disruptions.
From proprietary GSM weights (40g to 80g) and custom color coding (green, blue, purple) to personalized private-label packaging and regulatory documentation support, we empower global brands to scale seamlessly.
Uncompromising quality control backed by global medical device certifications.
Every batch of disinfection wrap undergoes rigorous burst strength testing, hydrostatic head water repellency tests, linting evaluation, and microbial penetration resistance assays before leaving our cleanrooms.
Manufactured under strict ISO 13485, ISO 9001, CE, and FDA-registered standards, ensuring seamless customs clearance and hospital tender approval across Europe, North America, Southeast Asia, and the Middle East.
Our 30+ automated lines allow us to handle massive volume orders with industry-leading lead times, ensuring distributors maintain optimal inventory turnover ratios.
Guangdong Onyx Medical operates under the guiding principles of "Technological Innovation, Quality First," striving to establish a strong brand presence in the global market. The company places a strong emphasis on quality control while ensuring that its production processes are sustainable. With a commitment to environmental protection, resource utilization, and social responsibility, Onyx Medical has gained a reputation as a trusted partner in the healthcare, personal care, and electronics industries. The company’s advanced research and development capabilities, coupled with its efficient production systems, continue to drive it forward as a key player in these sectors. Moving forward, Onyx Medical is dedicated to pushing the boundaries of material science, providing innovative and efficient solutions for its customers worldwide.
Complete your sterile processing sterile barrier system with our comprehensive manufacturing catalog.
Expert insights for global procurement managers and hospital central sterile services departments (CSSD).
Medical-grade SMS (Spunbond-Meltblown-Spunbond) wraps are engineered in Class 100,000 cleanrooms to provide a multi-layer barrier system. The meltblown core acts as a high-efficiency filter against bacteria and particulates, while the outer spunbond layers deliver high tensile strength, puncture resistance, and drapability, specifically validated for steam, EO, and plasma sterilization processes.
Yes. As a leading manufacturer with over 60,000 m² of production space and 30+ automated lines, we offer full OEM/ODM customization including specific GSM weights (45g to 80g), custom sheet dimensions, private label printing, and specialized color coding tailored to regional hospital standards.
Our manufacturing facilities and products comply with strict international benchmarks, holding ISO 13485 medical device quality management certification, ISO 9001, CE marking, and FDA registration, ensuring smooth regulatory compliance for importers and healthcare institutions worldwide.
Thanks to our automated PLC-controlled production lines and robust raw material inventory, standard bulk orders are typically fulfilled and ready for dispatch within 15 to 25 business days, backed by comprehensive logistics support to major global ports.
 Onyx Medical